A spark detection and extinguishing system is an automatic industrial protection system that detects moving ignition sources in a process stream and triggers an extinguishing response before they reach vulnerable downstream equipment. We recommend evaluating it where sparks or embers can travel toward dust collectors, filters, or silos. The right configuration depends on the material, conveying conditions, detection coverage, available installation distance, and extinguishing-medium compatibility.
The key decision is whether the complete system can detect and intercept the relevant ignition source under your actual operating conditions. A fast detector alone is not enough. Water-based extinguishing must suit the material, and response timing must match the layout. Spark control also does not replace explosion venting, suppression, or isolation where the risk assessment requires those measures. Start with the process hazard and protection objective, then confirm the equipment and installation.
It addresses transported ignition sources that could ignite combustible material farther along the process. Typical concerns include sparks, glowing embers, and, with suitable detection technology, other hot particles. The protection objective is to interrupt that travel path before the source reaches a vulnerable accumulation or process zone.
Grinding, cutting, friction, tramp-metal impact, and overheated equipment can introduce hot material into extraction or conveying systems. Whether that material causes ignition depends on its characteristics and the receiving environment. A dust fire and a dust explosion are related hazards, but they are not the same event.
We would map the source, transport path, and downstream equipment before discussing detector quantity. For a wider explanation of the hazard chain, see our guide to common causes of dust collector explosions. A system on one inlet does not automatically protect every route into a collector.

The system links detection to a controlled extinguishing action while the ignition source is moving. In a typical water-based arrangement, the particle travels into a spray zone downstream of the detector. Detection, control, valve actuation, and effective spray formation must be evaluated together.
Optical detectors monitor a defined part of the material path. Their suitability depends on the radiation they detect, viewing geometry, contamination, and process conditions. A device intended for glowing sparks should not be assumed to detect every non-glowing hot particle.
The controller commands the extinguishing assembly according to the configured logic. Water is released through selected nozzles to intercept and cool the target particles. Nozzle coverage, water delivery, and activation duration must suit the installation; a signal to open a valve is not proof that adequate water reached the duct.
The response can include notification, event recording, and process interlocks. Continued or repeated detections may require a different action from an isolated event. We recommend defining those actions before commissioning so operators know when to investigate, stop equipment, or follow an emergency procedure.

A complete installation combines sensing, control, extinguishing, utilities, and supervision. These elements must be specified as one functional chain. Buying compatible-looking components separately does not establish that the assembled system will perform as required.
| Element | Purpose | What to confirm |
|---|---|---|
| Spark detectors | Identify relevant moving ignition sources. | Detection capability, coverage, ambient light, and process temperature. |
| Control panel | Receive signals and initiate defined actions. | Zone logic, event records, interfaces, and fault handling. |
| Extinguishing assembly | Deliver the extinguishing medium. | Nozzle arrangement, valve performance, coverage, and compatibility. |
| Water supply | Support the required discharge. | Available pressure and flow, water quality, and freeze protection. |
| Supervision and interfaces | Report relevant faults and coordinate the process. | Included monitoring, alarm routing, power behavior, and restart conditions. |
Confirm what is included, optional, and supplied by others. A quotation may cover detectors and a panel while leaving the booster package, site wiring, piping, or commissioning outside its scope. Those boundaries affect both cost and readiness for operation.
Spark detection is worth assessing where combustible material can carry ignition sources toward vulnerable equipment. Wood processing, biomass handling, recycling, and selected food or textile processes are examples. Industry labels alone are not enough to establish suitability.
Review each inlet, branch, fan position, and protected destination. Changing the transport route or adding a machine can change the protection arrangement. A mechanical transfer point also needs its own coverage assessment rather than a layout copied from an enclosed duct.
Material can shield a hot particle from a detector's view. Background radiation, process heat, and external light may also affect detector selection. Ask for evidence covering the relevant target and conditions instead of relying on the general phrase “infrared detection.”
Water is not suitable for every material or process. Water-reactive materials require a different assessment, and moisture-sensitive products may present quality or handling constraints. Spark detection in a transport line also does not establish protection against an existing deep-seated fire, every electrical ignition source, or a thermal event elsewhere in the facility.
Spark detection and extinguishing targets an ignition source moving through a defined path. Explosion suppression acts on a developing explosion, while venting and isolation address other parts of the protection strategy. These functions should be coordinated, not treated as interchangeable product choices.
| Method | Primary objective | Important boundary |
|---|---|---|
| Spark detection and extinguishing | Detect and extinguish transported ignition sources. | Performance depends on the source, coverage, response, and extinguishing conditions. |
| Mechanical spark arrestor | Separate or capture certain particles. | Performance depends on design and particle conditions; it is not equivalent to active detection. |
| Explosion suppression | Detect and suppress a developing explosion. | Requires a design matched to the dust, equipment, and explosion scenario. |
| Explosion venting | Relieve explosion pressure through a designed opening. | Needs appropriate sizing, discharge arrangements, and equipment assessment. |
| Explosion isolation | Limit explosion propagation through connections. | Depends on device suitability, location, direction, and operating conditions. |
For the supporting layers, read what an explosion venting panel does and how explosion isolation flap valves work. Where flameless venting is being considered, our flameless explosion venting selection guide explains why location and application limits still matter.

Selection starts with the material and operating envelope, then checks whether the proposed equipment and layout can meet the protection objective. We would review normal operation, startup, shutdown, and credible changes in flow. A design based only on average operating conditions can miss important constraints.
Identify particle characteristics, loading, moisture, temperature, and available combustible-dust test data. Explain whether the flow is steady or intermittent and whether contaminants are expected. These details inform detection and extinguishing decisions, but no single dust parameter determines the entire design.
The available travel time must allow the system to establish an effective extinguishing zone before the target arrives. Conveying speed, particle behavior, controller and valve delays, and water delivery all influence the assessment. There is no universal detector-to-nozzle distance for every system.
Use the selected product's current installation manual and project-approved drawings. Check straight lengths, branches, elbows, detector orientation, access, and the protected destination together. Generic timing logic must not be used to reduce a manufacturer's specified installation spacing.
Confirm water availability during the required operating states, including the effects of filters, pipe losses, and other water users. Review freezing exposure, drainage, maintenance access, power supply, and the agreed fault response. Installation work, commissioning, spares, and recurring inspections can materially change the total project cost.
Planning a Retrofit or a New Conveying Line?
Share the material, duct layout, conveying conditions, and available water supply with BasCo. These inputs help define the review before you request a final configuration.

Testing should demonstrate the agreed functional chain, including alarms and process interfaces. Maintenance should preserve those functions throughout service. The inspection and test schedule must follow the selected equipment documentation, site conditions, and applicable requirements.
Verify the installed arrangement against approved drawings and identify each protected zone. Use the manufacturer's approved test methods to check detection, control outputs, extinguishing delivery, monitoring, and interlocks. Controlled tests should be planned with the site; introducing a live ignition source into an operating dust process is not an acceptable informal check.
Inspect the relevant viewing surfaces, nozzle condition, water supply, valves, and monitoring functions. Confirm how loss of power, low water pressure, or another detected fault is reported and handled. Do not assume a panel fault automatically stops production unless that behavior is specified and verified.
Repeated activations deserve investigation of the upstream cause, not just repeated resetting. Keep test results, faults, cleaning work, and corrective actions traceable. Reassess the arrangement after changes to machines, material, duct routing, operating speed, or control logic.
The applicable documents depend on the project location, adopted requirements, hazard assessment, insurer, and equipment scope. Confirm the required editions at the start. A product certificate and an installed-system acceptance record answer different questions.
For projects using NFPA references, NFPA 660 brings together combustible-dust requirements previously covered by several separate standards, including NFPA 652 and NFPA 664. NFPA 69 addresses explosion prevention systems. Older project specifications may still name legacy documents, so the project team should resolve the governing basis rather than simply replacing references in a quotation.
Ask for the configuration-specific manual, drawings, applicable certificates or approvals, commissioning procedure, maintenance instructions, and interface schedule. For hazardous-area equipment, verify that the marking and documentation match the installation environment. Do not infer a whole-system approval from one certified component.
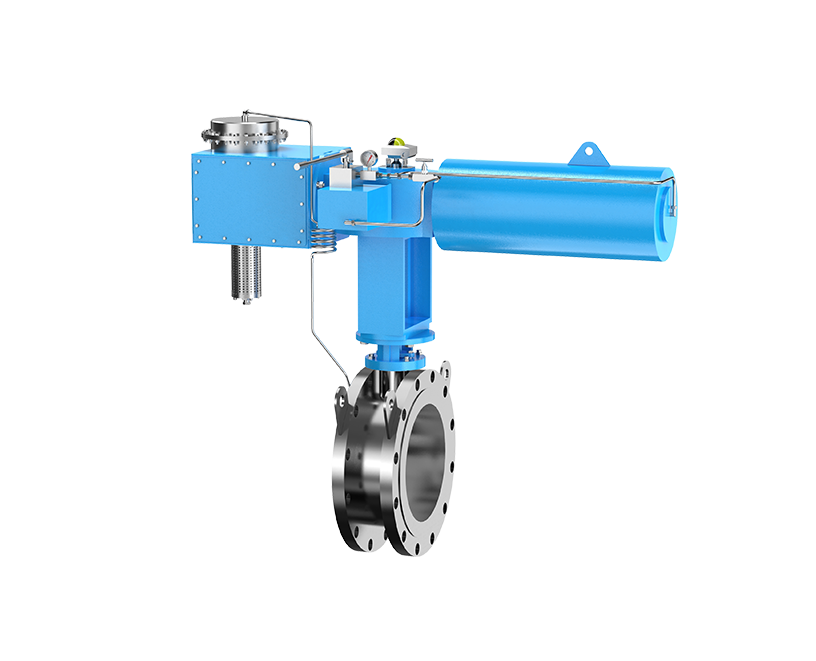
The BasCo 3100 and 3200 address different stages of the hazard chain. The 3100 Spark Detection & Extinguishing System is the relevant starting point for transported ignition-source control. The 3200 Explosion Suppression System addresses a developing explosion and requires a separate application assessment.

Explore BasCo's system for detecting and extinguishing ignition sources in a process transport path. Confirm the current detector arrangement, installation requirements, water supply, and control interfaces for your application.
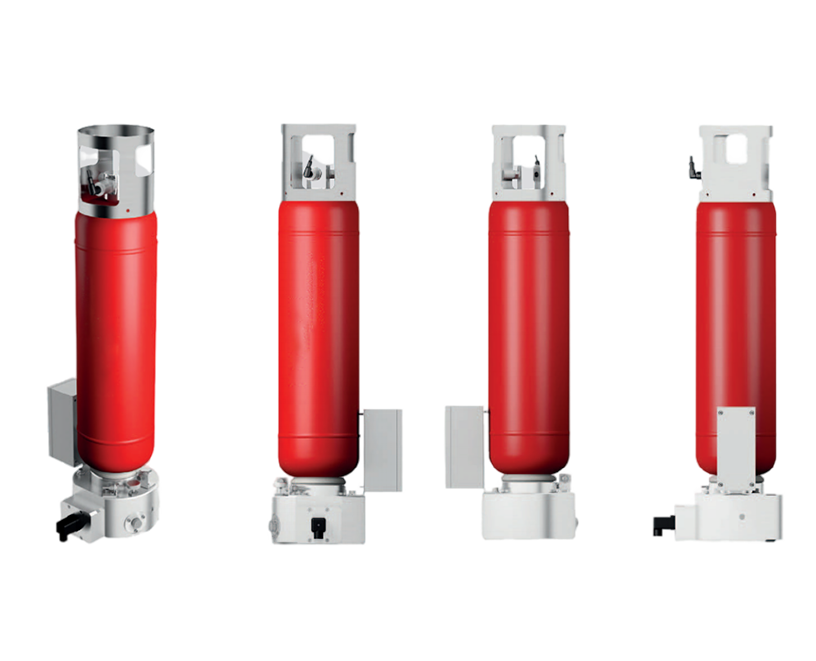
Explore BasCo's system for suppressing a developing explosion in industrial equipment. The configuration must be reviewed against the protected equipment, dust characteristics, operating conditions, and required performance.
Send enough information for the supplier to evaluate the process and define the supply boundary. A request for “one spark detector” leaves major questions unanswered. We recommend attaching a marked layout and the available material data.
| Information | Include in your request |
|---|---|
| Material and hazards | Material identity, particle characteristics, moisture, temperature, contaminants, and available dust test or hazard-assessment data. |
| Transport and layout | Duct dimensions, operating range, branches, elbows, fan positions, available straight lengths, and downstream equipment. |
| Utilities and environment | Water pressure and flow data, water quality, power supply, ambient conditions, and hazardous-area information. |
| Actions and integration | Alarm destinations, stop or diversion requirements, control interfaces, existing protection, and restart responsibilities. |
| Scope and acceptance | Design, hardware, piping, wiring, installation, commissioning, training, documentation, spares, and acceptance responsibilities. |
Compare quotations against the same scope. Clarify who confirms the final layout and who verifies the installed response. A lower equipment price can exclude the engineering or site work needed to make the protection functional.

Some detector technologies are designed for this task, but the capability is not universal. Confirm the target characteristics, viewing conditions, and documented performance of the proposed detector.
It may continue where the application and approved response logic allow it. Repeated detections, supply faults, or other conditions may call for shutdown or another action. Define the decision and restart process in advance.
It does not automatically remove those requirements. Transported ignition-source control cannot cover every ignition scenario. The hazard assessment must determine the remaining explosion protection and isolation needs.
No. Material reactivity, product quality, equipment compatibility, and process conditions must be checked. Where water is unsuitable, the protection concept needs a separate review rather than a different nozzle chosen by default.
The selected system requirements, transport conditions, complete response chain, and available geometry determine the arrangement. Obtain an application-specific layout and follow the current installation manual.
The number of zones, detection requirements, water package, interfaces, site work, documentation, and commissioning scope all contribute. Compare installed and maintainable solutions rather than detector prices alone.
We recommend starting with a clear map of the ignition source, transport path, and vulnerable equipment. Then confirm detection capability, effective extinguishing, installation constraints, and the response to faults. The useful purchase is a documented protection function that fits the process.
If you are assessing a new line or an existing installation, share your material data and layout with BasCo. We can use that information as the starting point for discussing the 3100 system and any separately required explosion protection measures.
Discuss Your Spark and Explosion Protection Requirements
Send your process layout, material information, and project scope. Start a focused discussion about ignition-source control, required protection layers, and the next technical review.

Where Are Rupture Disks Used in Chemical and Petrochemical Plants?
2026-09-21Burst Pressure Tolerance Explained: How Accurate Are Rupture Disks?
2026-09-16Full-Process Quality Control for Rupture Discs
2026-09-01Rupture Disk Selection Guide: How to Choose the Right Type, Pressure, Material, and Size
2026-08-25Copyright © Jiangsu Bafang Safety Device Co., LTD. All Rights Reserved